Case Studies
Featured Project8 Multi-Burner Natural-Draft Process Heater Upgrades
Project Overview
Trecora needed to modernize 8 aging direct-fired process heaters that were becoming harder to operate, troubleshoot, and support. Profire delivered an API-aligned PF3100-based burner management and controls upgrade with data and event logging, control room visibility, and integration into the existing plant infrastructure. The solution also established a repeatable path for future heater upgrades across the site.
Project Highlights
- Problem
 8 aging heaters drove maintenance burden
- Limited visibility and API supportability
- Solution
- PF3100-based burner management controls upgrade
- Data/event logging with Modbus and DCS integration
Recent Projects
Oil & Gas – Upstream
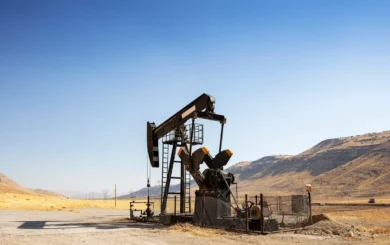
148-Unit Horizontal Heater Treater Retrofit
Project Highlights
See Details
- Problem
- 148 aging units relied on manual lighting
- Frequent downtime, callouts, and truck rolls
- Solution
- PF2200-DB retrofit with M7 Burner upgrades
- Auto re-light, data logging, SCADA visibility
Oil & Gas – Downstream / Utility
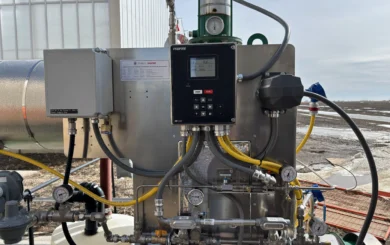
Tecvalco CWT Vacuum Heater Retrofit
Project Highlights
See Details
- Problem
- Legacy controls required relights
- Limited heater visibility
- Solution
- PF2200-SB BMS integration
- Vacuum tracking added
Chemical & Petrochemical
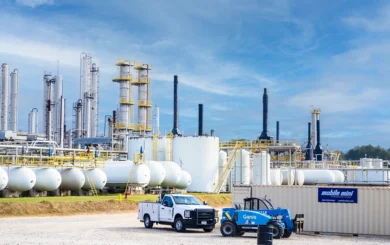
8 Multi-Burner Natural-Draft Process Heater Upgrades
Project Highlights
See Details
- Problem
- 8 aging heaters drove maintenance burden
- Limited visibility and API supportability
- Solution
- PF3100-based burner management controls upgrade
- Data/event logging with Modbus and DCS integration

Oil & Gas – Midstream
6 Large Hot Oil Heater Control Upgrades
Project Highlights
See Details
- Problem
- 6 x large-BTU heaters needed safe control
- Needed plant-wide controls integration
- Solution
- 6 x PF3100 BMS Controllers
- Fuel-air ratio with VFD feedback

Oil & Gas – Midstream
Triple-Tube Line Heater Automation
Project Highlights
See Details
- Problem
- No auto recovery after light-off failures
- Limited visibility between operator rounds
- Solution
- Auto re-light using PF2200-based controls
- 3-burner setpoint control with load sharing
Biogas
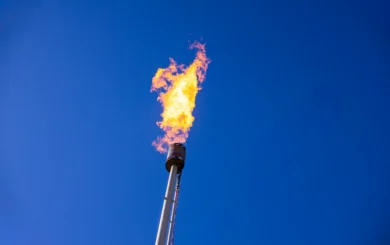
Chestnut Valley Candlestick Flare Control Package
Project Highlights
See Details
- Problem
- Brand new flare system required
- Faced compliance risks under strict EPA regulations
- Solution
- New candlestick flare w/ PF3100 BMS controller
- FSI pilot ignition system w/ dual flare-top sensors

Landfill
Dual Candlestick Flare for RNG Facility Expansion
Project Highlights
See Details
- Problem
- Unable to support increased gas volumes
- Faced compliance risks under strict EPA regulations
- Solution
- Dual candlestick flares w/ 12,000 SCFM capacity
- Two PF2100F flare controllers w/ auto/on-demand ignition

Food & Beverage
Low Temperature Spray Dryer
Project Highlights
See Details
- Problem
- Unable to maintain process temperature below 41°C (105.8°F).
- Low visibility required hands-on checks
- Solution
- PF3100 held temps below 41°C (105.8°F)
- Modbus & logging added real-time insight

Oil & Gas – Midstream
Forced Draft TEG Reboiler
Project Highlights
See Details
- Problem
- Faced severe regulatory fines
- Emitted >70 ppm NOx & 400 ppm CO
- Solution
- Reduced NOx <20 ppm & CO <1 ppm
- Achieved 20% natural gas savings

Oil & Gas – Downstream / Utility
Line Heater Upgrade
Project Highlights
See Details
- Problem
- Lacked auto ignition and safety shutoff
- Improper burner setup caused frequent blow outs
- Solution
- Installed two PF2100s for safe operation
- Improved airflow for complete combustion

Oil & Gas – Midstream
Main Burner Upgrade
Project Highlights
See Details
- Problem
- Lacking a standalone pilot system.
- Hazardous ignition system risking equipment and personnel.
- Solution
- High-efficiency pilot for reliable repeatability.
- Mitigated hazards involving competitor products.

Reclamation
Dual Pilot Forced Draft Flare
Project Highlights
See Details
- Problem
- Required manual ignition
- Unable to monitor pilot or flare status
- Solution
- Real-time data cut service callouts
- Automated the pilot ignition system

Oil & Gas – Midstream
12 Burner Hot Oil Cabin Heater
Project Highlights
See Details
- Problem
- Required manual ignition
- Unreliable flame detection & monitoring
- Solution
- Auto ignition delivered 30% fuel savings
- Remote monitoring for 40+ safety inputs

Oil & Gas – Upstream
Amine Distillation – Cabin Heater
Project Highlights
See Details
- Problem
- Flame failures caused 3+ daily shutdowns
- Operators had to manually re-light
- Solution
- Auto relight & temp control saved 45% fuel
- Reliable monitoring of 250+ safety inputs

Oil & Gas – Midstream
120gpm Amine Plant Boiler Upgrade
Project Highlights
See Details
- Problem
- Lack of controls forced manual operation
- Uneven air-fuel ratio hurt performance
- Solution
- Advanced controls improved output
- NFPA 87-compliant trains & safety logic

Oil & Gas – Upstream
Pre-packaged Systems for BMS Retrofits
Project Highlights
See Details
- Problem
- Variable BMS setups created unsafe conditions
- System reliability varied by appliance
- Solution
- Upgraded 200+ appliances with new system
- Achieved ~2 hours downtime per upgrade

Power Generation
Vacuum Boiler – Natural Gas Line
Project Highlights
See Details
- Problem
- Unable to keep temps below 41°C (105.8°F)
- Low visibility required hands-on checks
- Solution
- PF3100 held temps below 41°C (105.8°F)
- Modbus & logging added real-time insight