Burner Management and Combustion Control for Midstream Oil & Gas Process Heating
In a gas processing plant, fired equipment carries the heat load for treating, dehydration, fractionation, and heat medium circulation. Midstream Oil & Gas burner management systems sequence ignition, supervise flame, and enforce safe shutdown on hot oil heaters, amine and NGL fractionation reboilers, station heaters, and combustors. Profire, a CECO Environmental brand, designs and supports the controls around that equipment, from the burner management system and fuel train through plant communications and commissioning.
Burner Management Systems for Midstream Fired Equipment
Fuel Trains for Gas Plant and Station Heaters
Burners and Air Control for Large Process Heat Loads

Midstream Oil & Gas Subindustries We Serve
-
 GAS PROCESSING & TREATING
-
 HEAT MEDIUM & HOT OIL SYSTEMS
-
 NGL RECOVERY & FRACTIONATION SUPPORT
-
 GAS GATHERING & PROCESSING
-
 PIPELINE TRANSMISSION & PRESURRE REGULATION
-
 STORAGE, TERMINALS & VAPOR MANAGEMENT
Why Midstream Oil & Gas Operations Choose Profire
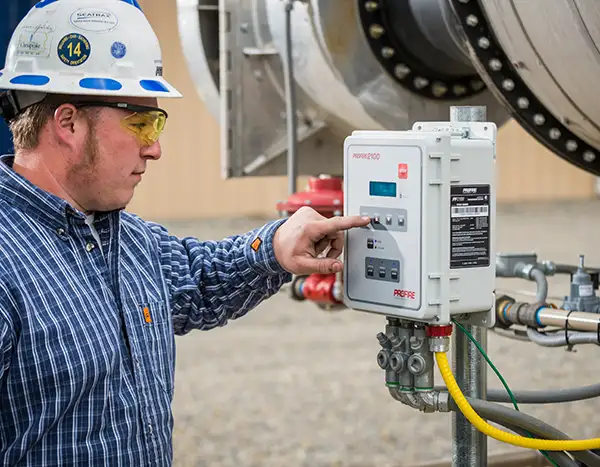
Safer Light-Off on Plant-Scale Heaters
Larger fired systems add purge timing, airflow proving, and more permissives to every start. Profire controllers sequence each step, prove pilot and main flame, and shut fuel off when flow, pressure, temperature, or flame conditions move outside range.
Plant & Station Visibility
Operators need to see a heater trip from the control room, not discover it on rounds. Profire controllers report burner status, first-out alarms, and event history over Modbus to DCS and SCADA, at the plant or at unmanned stations.
Stable Combustion for Critical Heat Loads
Hot oil and reboiler duty swings with plant throughput. Fuel/air ratio control, PID temperature control, and load sharing across multiple burners help heaters hold setpoint as demand changes, without overfiring the coil.
Support from Retrofit to Commissioning
PF2200 covers single burner, dual burner, and forced draft heaters, and PF3100 handles multi-burner, multi-pilot, and fuel/air ratio applications. Recent midstream retrofits include standardizing eight varied fired units on PF3100, with fuel trains rebuilt to NFPA 87.
Midstream Oil & Gas Fired Equipment Profire Supports
HOT OIL HEATERS / HEAT MEDIUM HEATERS
LINE HEATERS / STATION HEATERS
Glycol Dehydrators / TEG Reboilers
ANIME REBOILERS / GAS TREATING HEATERS
NGL FRACTIONATION REBOILERS
FUEL GAS HEATERS / CONDITIONING HEATERS
COMBUSTORS / ECDS / VDUS
Flares & Flare Ignition Systems
MIDSTREAM OIL & GAS FREQUENTLY ASKED QUESTIONS
What is process heating used for in Midstream Oil & Gas?
Process heating helps midstream operators treat, dehydrate, condition, fractionate, transport, and store natural gas, NGLs, and liquids, and manage vapors. In gas processing plants, that heat comes from hot oil and heat medium heaters, amine and NGL fractionation reboilers, and fuel gas heaters. Transmission and storage sites rely on station heaters, combustors, and flares.
Where are burner management systems used in midstream gas processing plants?
In a gas processing plant, burner management systems are typically found on hot oil and heat medium heaters, TEG and amine reboilers, NGL fractionation reboilers, and fuel gas heaters. Compressor stations, transmission sites, and terminals add station heaters, combustors, ECDs, VDUs, and flares. Each needs controlled ignition, flame supervision, temperature control, and a safe shutdown path.
Why do hot oil heaters need reliable burner management?
A single hot oil heater often supplies treating, dehydration, and fractionation at once, so one trip can affect several units. The heater also depends on thermal fluid moving through the coil. A burner management system proves flame, acts on low-flow and high-temperature shutdown inputs, and stops firing before a flow loss can overheat the coil or degrade the fluid. See the six-heater PF3100 upgrade.
Why do amine and NGL fractionation reboilers need stable heat input?
Amine reboilers regenerate the solvent that strips H<sub>₂</sub>S and CO<sub>₂</sub> from the gas, and fractionation reboilers drive separation in each NGL column. Too little heat leaves the product or solvent off spec. Too much, or uneven firing, can overheat tubes and degrade the amine. Whether the reboiler is direct-fired or heated by a hot oil system, stable burner control keeps it inside that window.
How does combustion control support gas processing operations?
Combustion control holds heat input steady as plant throughput changes, which keeps reboiler and heat medium temperatures where treating and fractionation need them. It also drives fuel use and emissions. In one published midstream project, combustion upgrades on a forced draft TEG reboiler cut NOx from above 70 ppm to below 20 ppm and reduced natural gas use by 20 percent.
Which Profire controller fits my midstream application?
For plant and station equipment, the choice is usually between PF2200 and PF3100. PF2200 covers single burner, dual burner, and forced draft heaters that need deeper diagnostics and data logging. PF3100 handles multi-burner and multi-pilot heaters, fuel/air ratio control, and plant-integrated systems such as large hot oil heaters. Natural draft station heaters may also fit PF2150. Compare the controllers side by side.
Can Profire support forced draft or multi-burner Midstream applications?
Yes. Profire supports natural draft, forced draft, single-burner, dual-burner, and multi-burner Midstream applications. These systems may require advanced burner management, fuel delivery, air control, flame detection, communications, and commissioning support.
Can Profire systems integrate with plant controls, DCS, or SCADA?
Yes. Profire burner management systems support Modbus communication with DCS, PLC, and SCADA systems, depending on the controller, configuration, and plant network. Operators can monitor burner status, first-out alarms, shutdowns, temperatures, and event history from the control room. Published midstream projects have paired PF3100 controllers with plant-wide controls integration and VFD feedback for fuel/air ratio control.
What midstream fired equipment does Profire support?
Profire supports midstream fired equipment such as hot oil and heat medium heaters, line and station heaters, glycol dehydrators and TEG reboilers, amine reboilers and gas treating heaters, NGL fractionation reboilers, fuel gas and conditioning heaters, combustors, ECDs and VDUs, and flares. At plant scale, controller selection usually turns on burner count, draft type, and how the heater ties into plant controls.
Tell us about your application
A Profire Specialist Will Contact You Shortly