148-Unit Horizontal Heater Treater Retrofit
Profire automated burner management across 148 aging heater treaters. Tell us more about your project
Project Highlights
- 148 dual-tube horizontal heater treaters retrofitted
- Automatic re-light replaced manual burner lighting
- Modbus integration with the existing SCADA system
- Designed to align with NFPA 87
- Reduced downtime, callouts, and truck rolls
- Upgrades helped the site qualify for a carbon credit
- 1.5 years from first contact to final commissioning
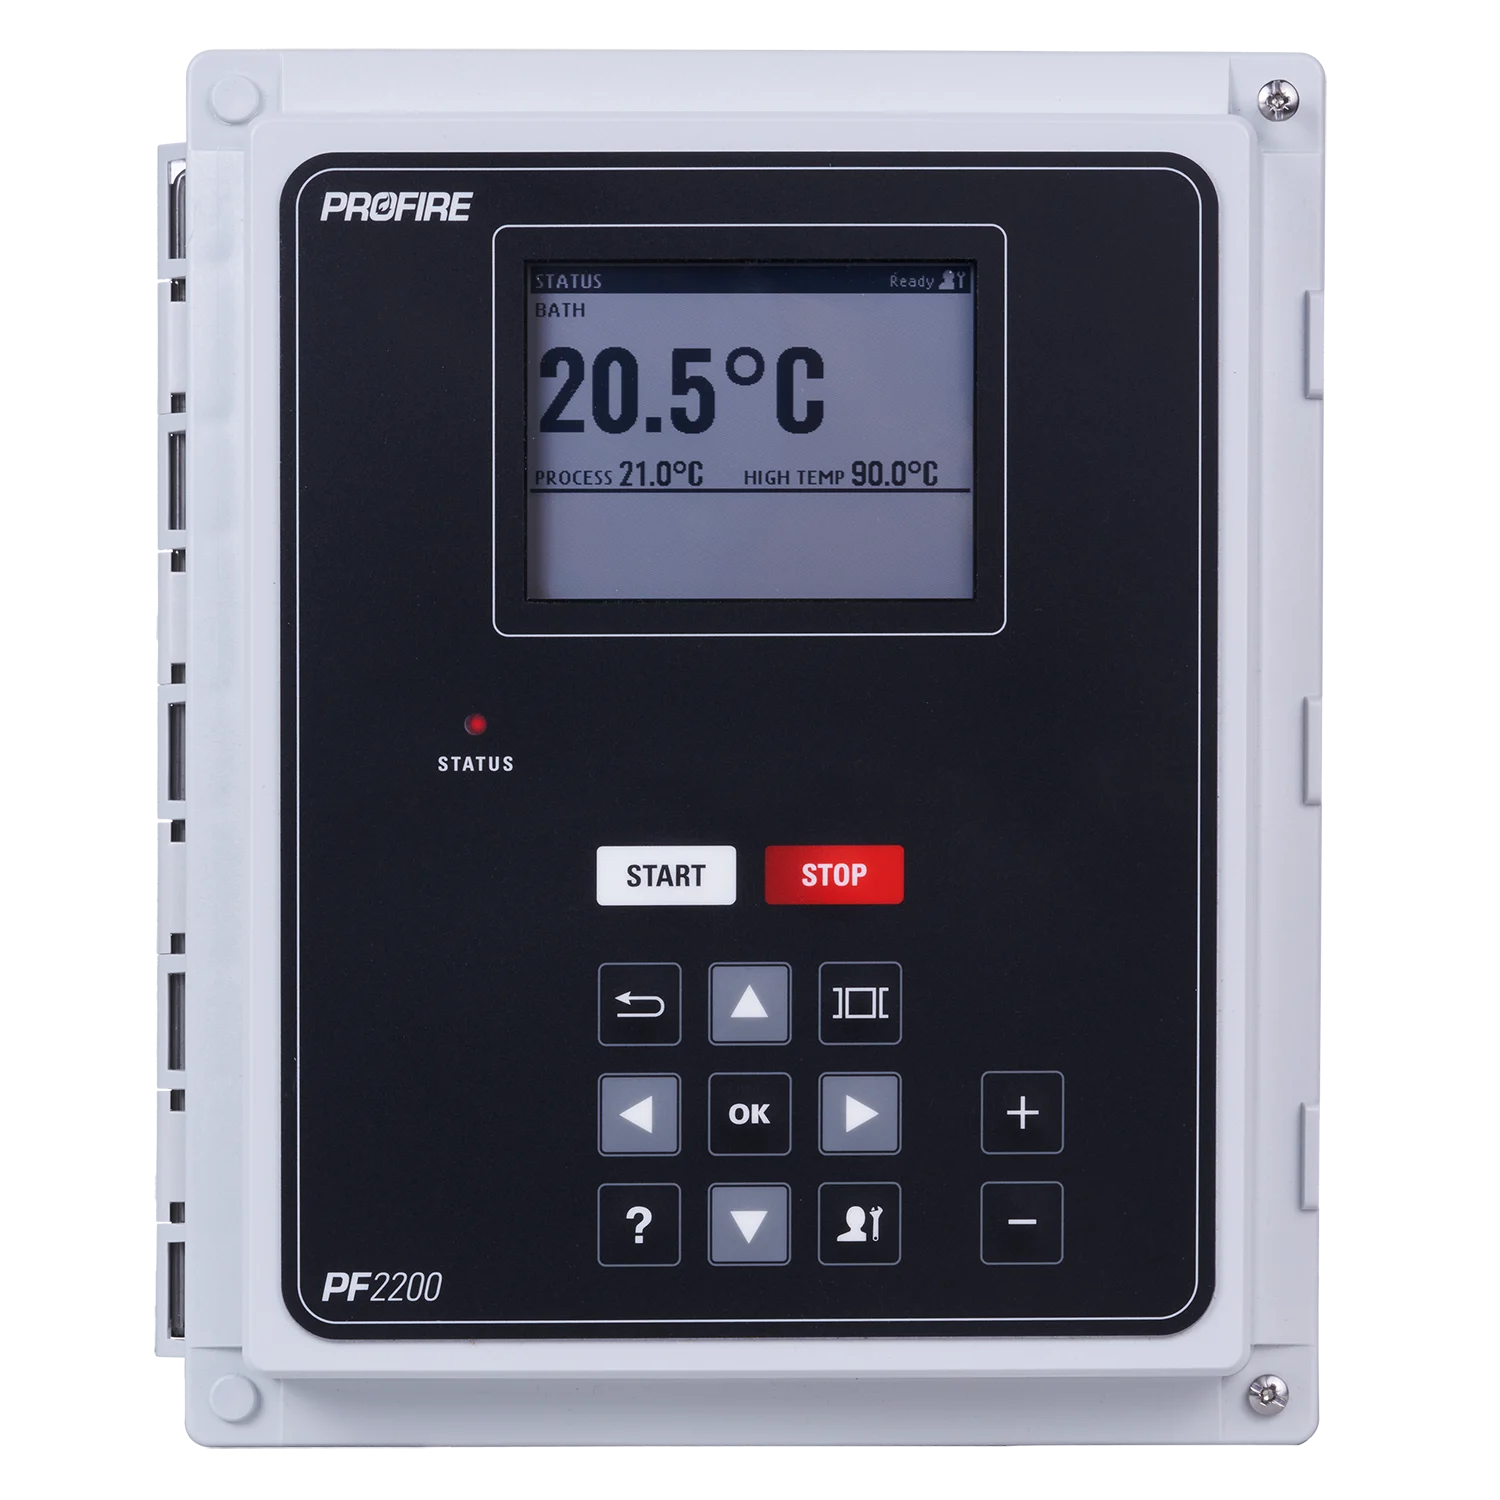
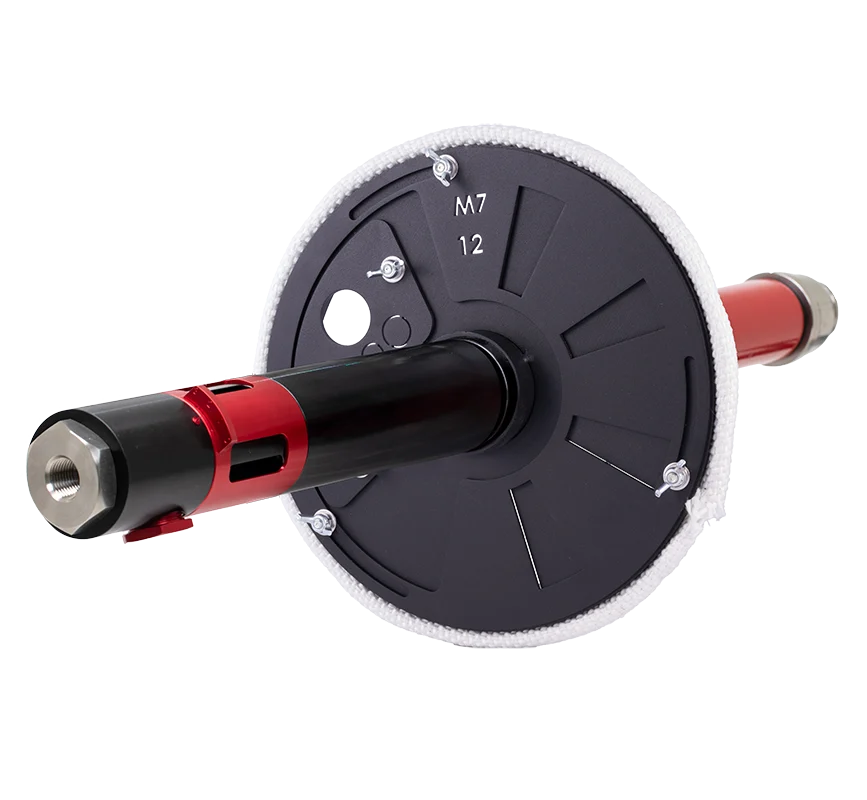
- PF2200-DB BMS Controller, 401AP fuel train, and M7 Burner per unit
The Problem
A leading Oil & Gas producer operated 148 aging dual-tube horizontal heater treaters running on pneumatic and manual controls. Operators lit burners by hand, and every flame failure meant a callout, a truck roll, and downtime until someone reached the site to relight the unit. Across 148 units, that burden added up fast.
New equipment arriving on site already featured modern burner management, and the customer’s engineering team pushed to bring the legacy units up to the same standard. The heater treater retrofits needed to align with NFPA 87 and be repeatable across a large equipment population without disrupting production.
Sound Familiar? Let's TalkBefore Profire
The Profire Solution
Profire delivered a standardized heater treater retrofit built around the PF2200-DB BMS Controller, a 401AP fuel train, and the M7 Burner with matched airplate and pilot. The units shared a common configuration, so no custom engineering was needed, and the same scope repeated cleanly across all 148 units.
Automated light-off and re-light replaced manual lighting. Data logging captured each unit’s operating history, and Modbus mapping tied the systems into the customer’s existing SCADA infrastructure so teams could check unit status from the office or control room.
Installation followed a simple rhythm. The customer’s electrical team wired a site one day, and Profire installed and commissioned the system the next. That cadence carried the program through all 148 units in 1.5 years.
Key elements included:
- PF2200-DB unit control: One controller and 401AP fuel train per heater treater
- M7 Burner upgrade: Matched airplate and pilot for better combustion efficiency
- Automatic re-light: No more manual lighting or waiting on a callout
- SCADA integration: Modbus mapping for control room visibility and data logging
- Installation & commissioning: All 148 units, with ongoing preventative maintenance
The Results:
Operators no longer light burners by hand, and units that once sat offline waiting for a technician now recover on their own. Downtime dropped, callouts and truck rolls fell, and the site’s problem children became easier to keep running. Crews get the job done quicker and get home sooner.
The M7 Burner and airplate upgrades improved combustion efficiency, and in December 2024 the installations helped the site meet a standard that qualified for a carbon credit. Profire continues to support the units through ongoing preventative maintenance.
Get a Free QuoteAfter Profire


Ready to Optimize your Equipment?
Let Profire help with your Safety, Reliability, and ESG Initiatives
Get a Free QuoteRecent Projects
Details
See Details
A leading Oil & Gas producer operated 148 aging dual-tube horizontal heater treaters running on pneumatic…
Details
See Details
At a natural gas utility site in Ontario, a installed Tecvalco CWT Vacuum Heater was exposed…
Details
See Details
Trecora operated 8 aging multi-burner natural-draft process heaters that were becoming harder to support. The heaters…