Retrofitting 8 Varied Fired Units on the PF3100 Platform
Fired equipment modernization on 8 varied fired units with a standardized PF3100 platform and control room communication. Tell us more about your project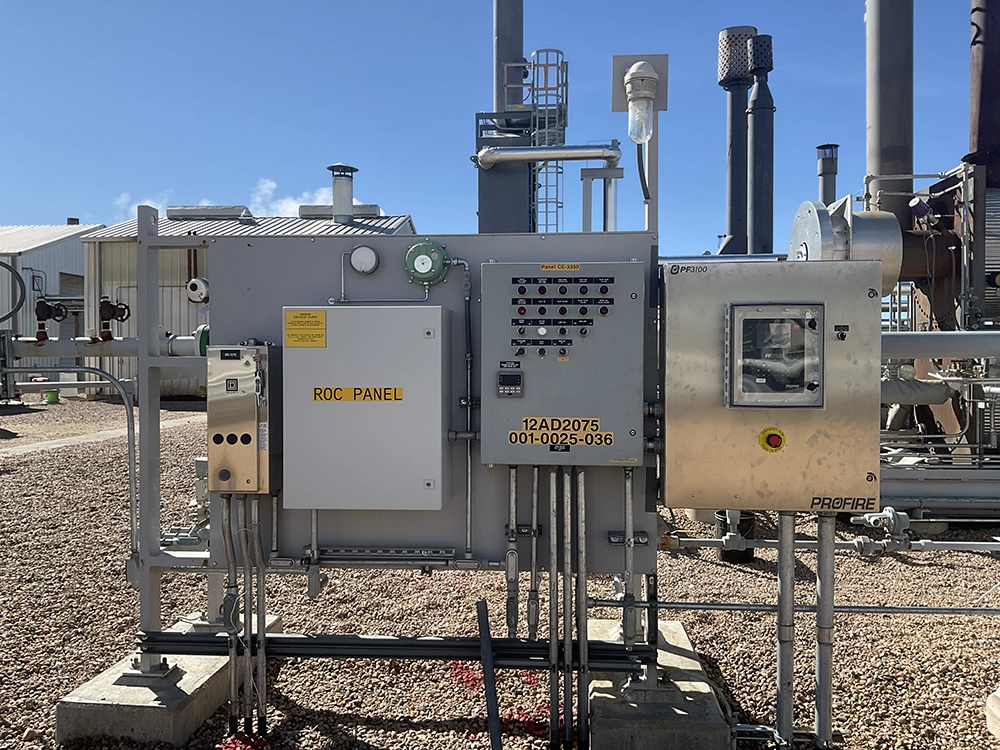
Project Highlights
- 8 varied fired units modernized under a single-source Profire scope
- 8 PF3100 BMS controllers standardized across every unit
- Fuel trains rebuilt or upgraded to current NFPA 87 code
- Modbus to SCADA communication to Western's control room
- One consistent operator interface and interchangeable spare parts across all heaters
- No nuisance shutdowns and no outstanding complaints reported after startup
- Profire delivered scope-out, mechanical work, commissioning, startup, tuning, and emissions reporting
- Full retrofit across cabin heaters, a cogen heater, thermal oxidizer, incinerator, and glycol dehydrators
The Problem
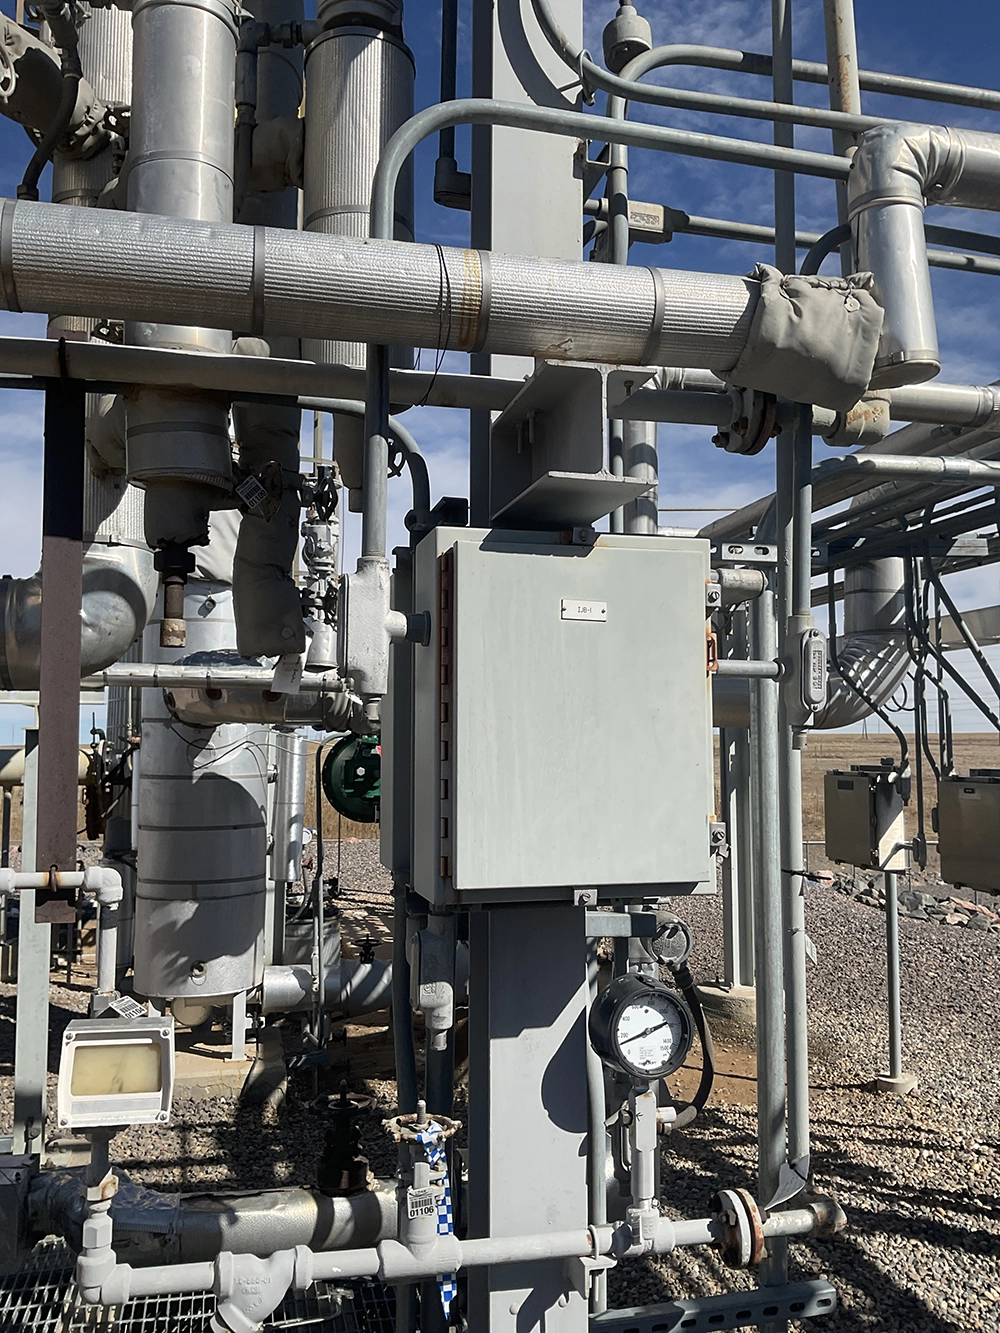
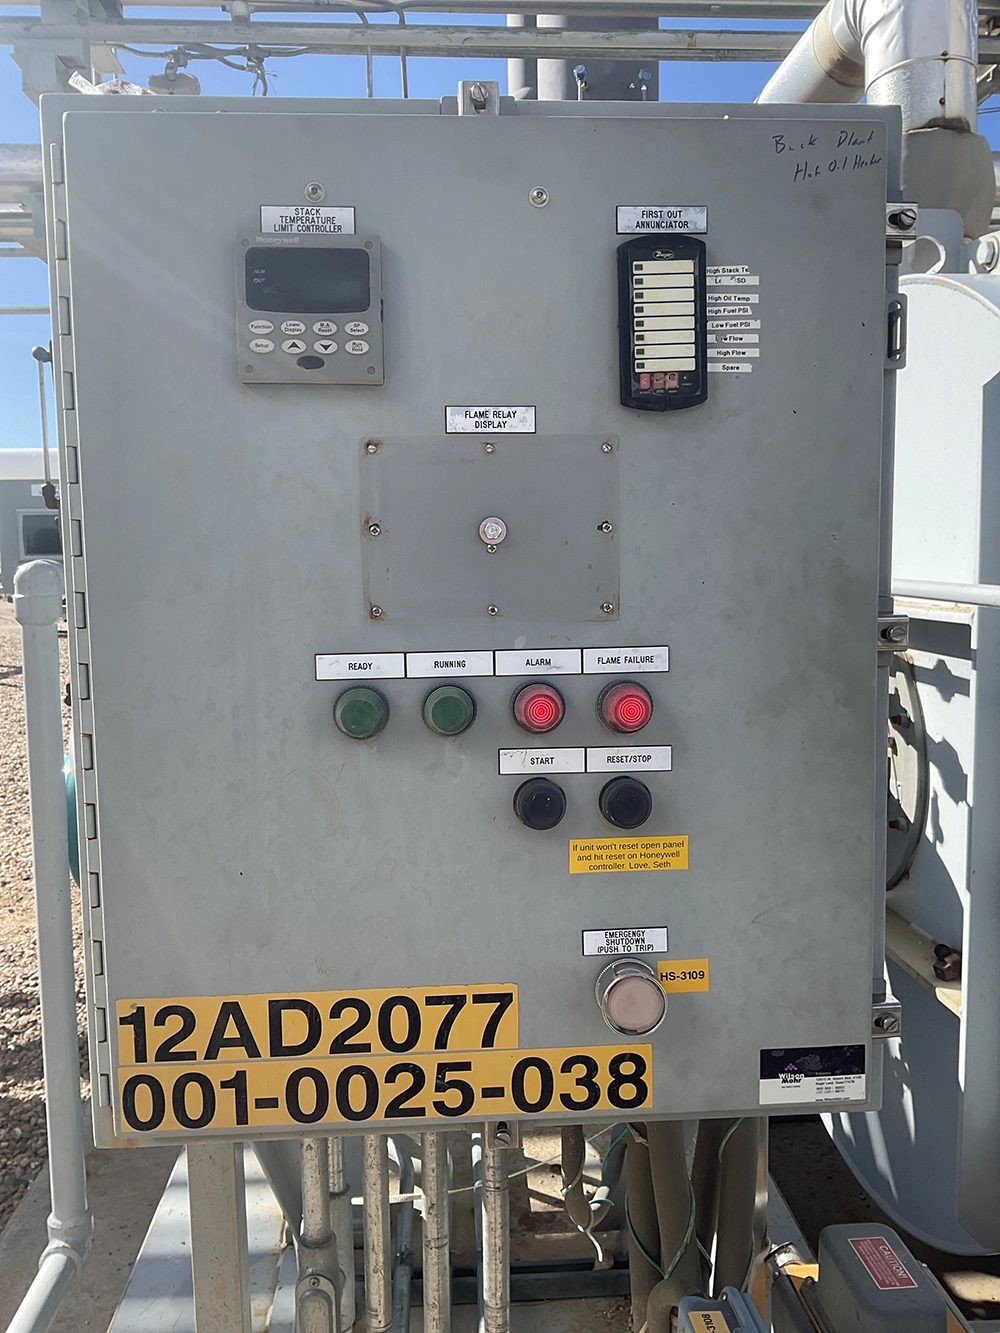
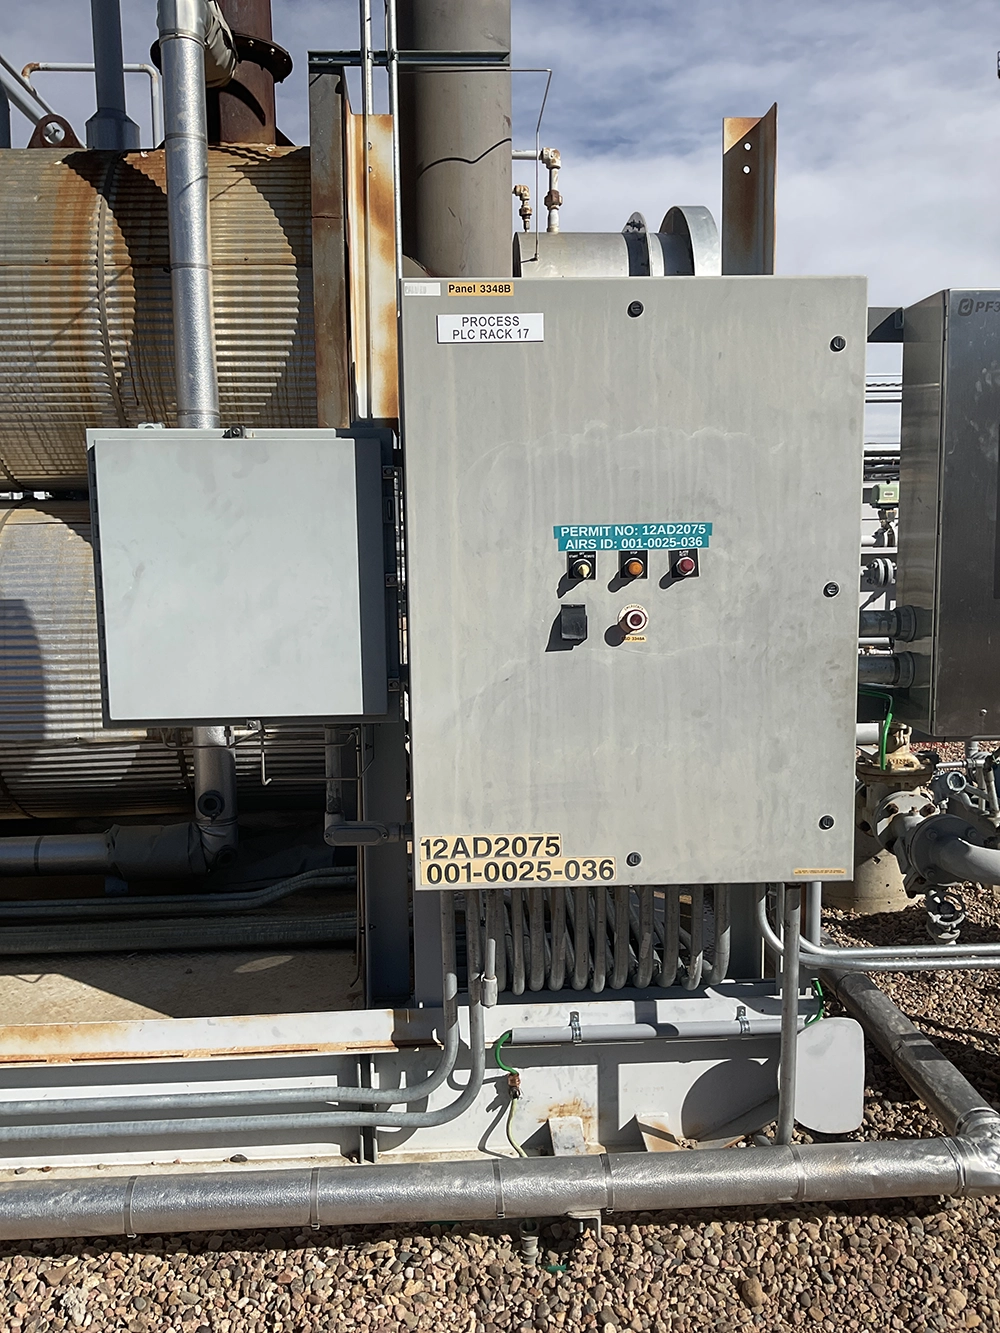
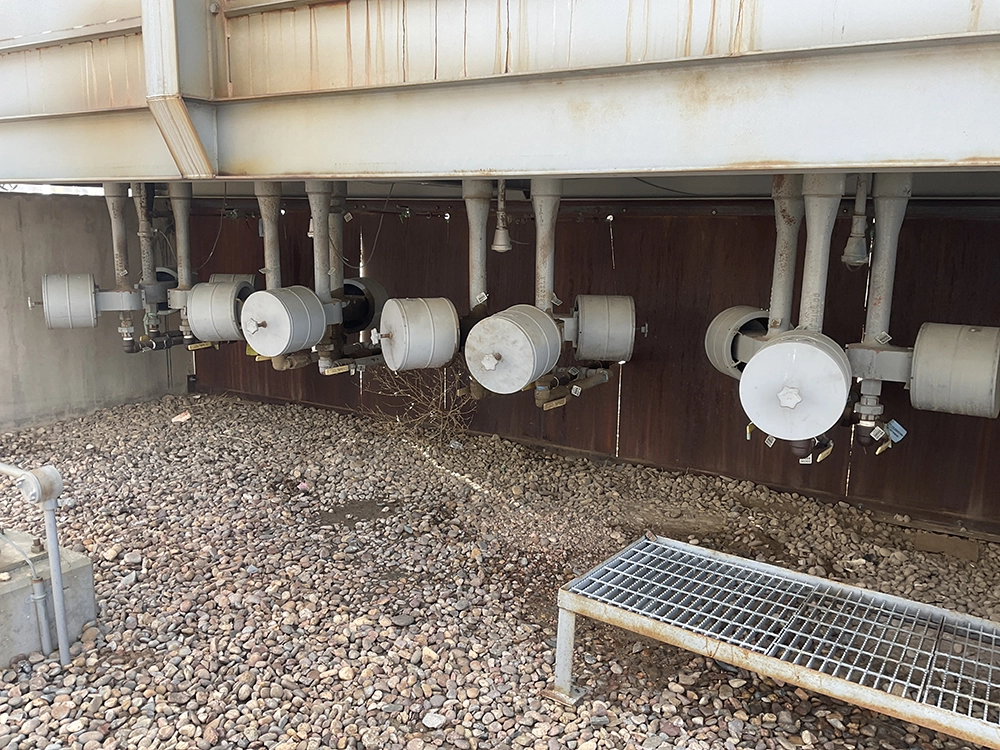
Western Midstream operates a natural gas processing plant near Denver, Colorado that had been running for roughly two decades. Over that time, the plant’s fired equipment and controls had aged into a patchwork of systems that were becoming harder to operate and support. Much of the control technology was around 15 years old and no longer reliable, and operators found the equipment increasingly difficult to work with day-to-day.
The pressure came from two directions at once. Colorado maintains some of the more stringent emissions requirements in the region, and Western needed its fired equipment to keep pace with those expectations. At the same time, the plant’s automatic relight function had become inconsistent. On many units it no longer worked as intended, which forced operators to go out and manually adjust a ball valve or regulator to bring a burner back into service. That hit-or-miss behavior varied from unit-to-unit and added avoidable field work.
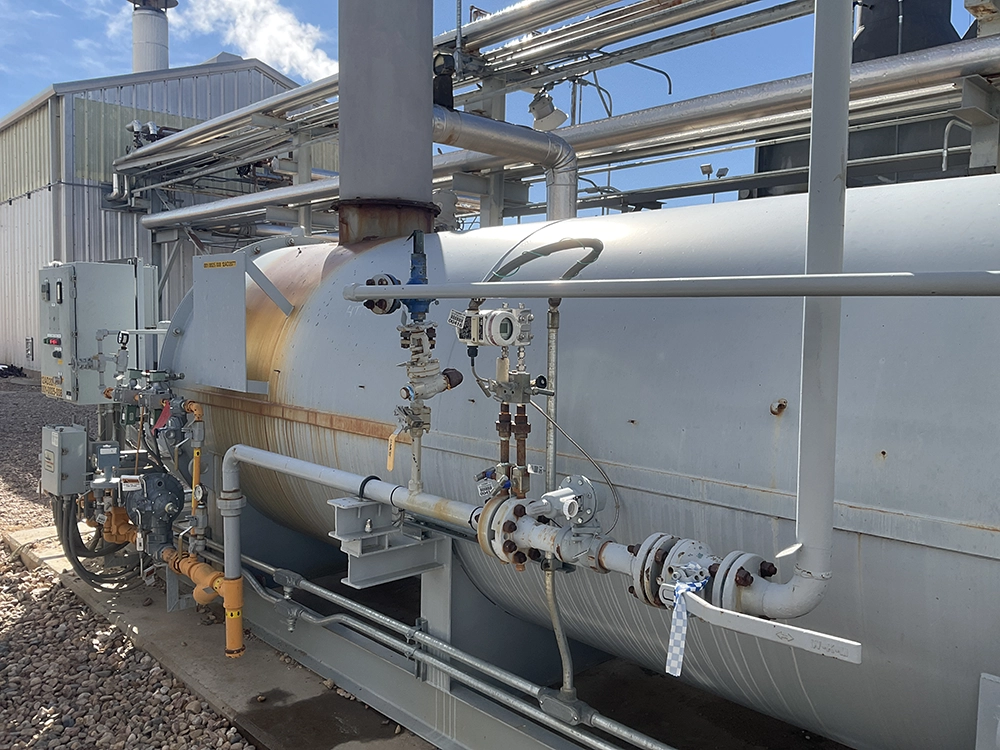
Complicating the picture was the variety of equipment. The plant relied on a mix of vessel types, from standard cabin heaters to a cogeneration heater, a thermal oxidizer, an incinerator, and glycol dehydrators, each with different operating principles. Modernizing all of them without a consistent control approach would have left operators managing a fragmented set of systems, spare parts, and procedures.
Sound Familiar? Let's TalkBefore Profire
The Profire Solution
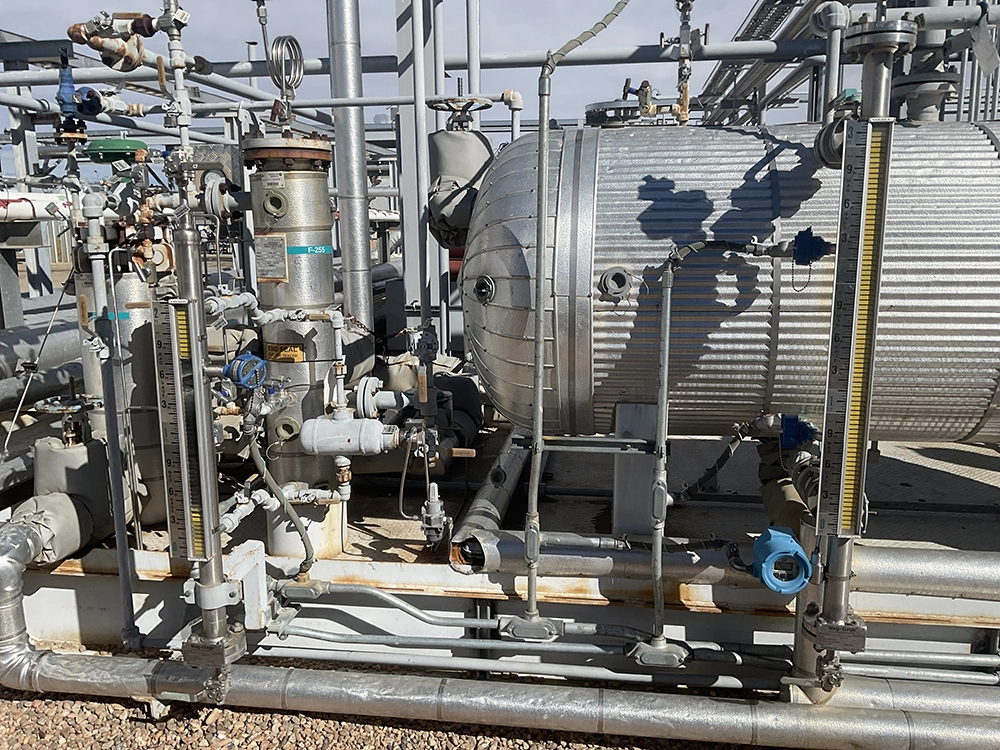
Profire delivered a single-source modernization that brought all 8 fired units onto one consistent control platform. After an initial scope-out of the plant, our team handled the work end to end, from mechanical modifications through commissioning, startup, tuning, and emissions reporting. The only element outside Profire’s scope was the site’s electrical work.
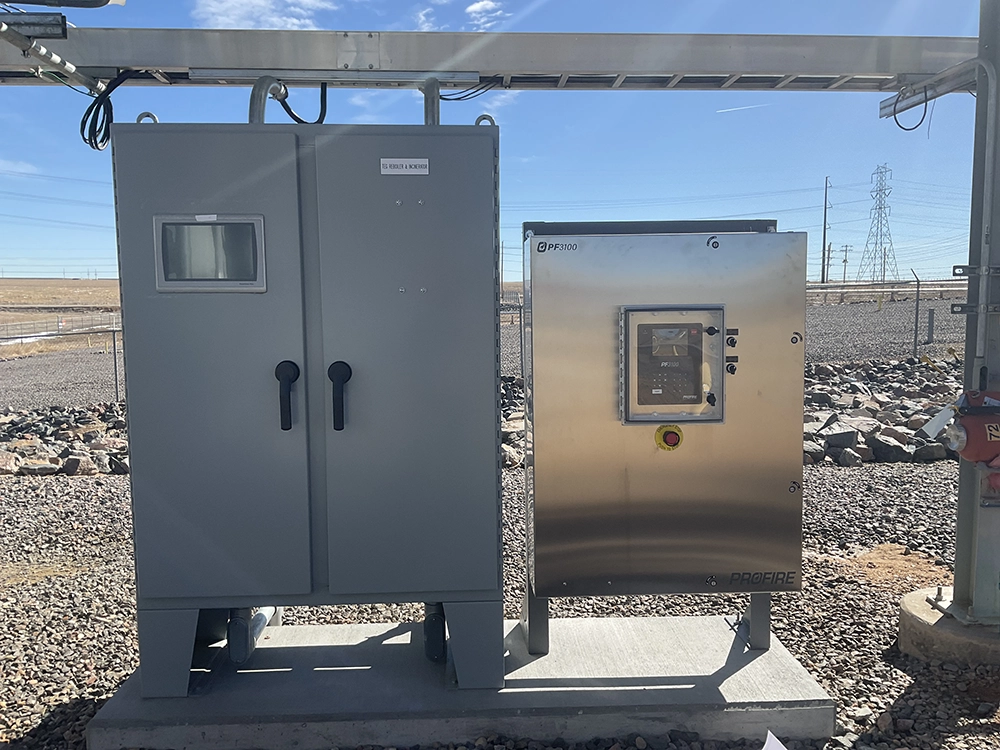
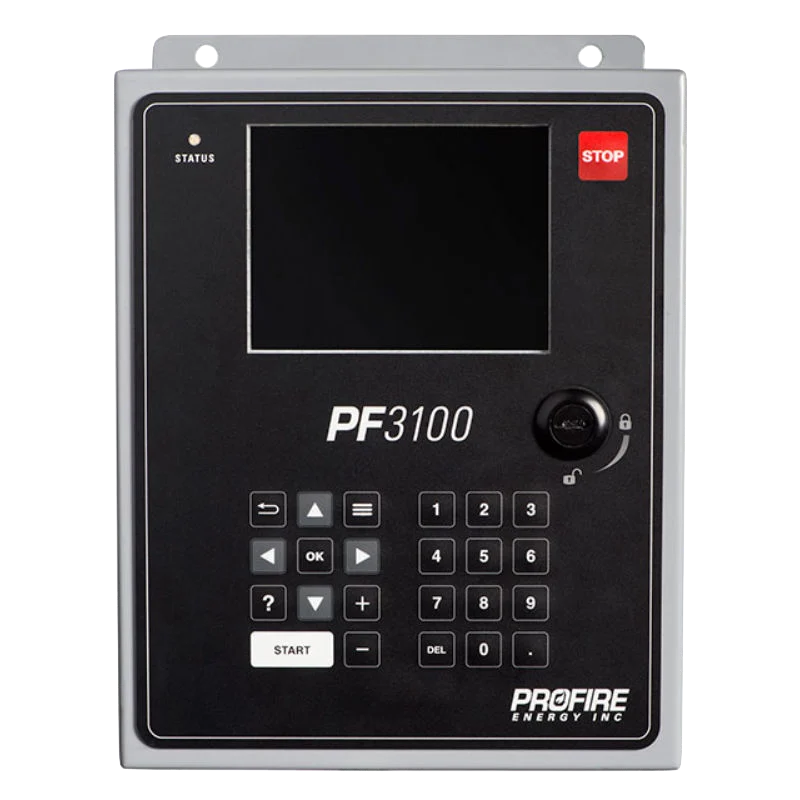
At the core of the upgrade were 8 PF3100 BMS controllers, one per unit. Standardizing on a single controller platform meant every heater, from the cabin heaters to the cogeneration heater, thermal oxidizer, incinerator, and glycol dehydrators, shared the same operator interface and underlying architecture, even though each vessel type followed different operating principles. That consistency simplified operation and made spare parts interchangeable across the site.
Key elements included:
- Standardized PF3100 platform: 8 PF3100 BMS controllers, one per unit, giving operators a consistent interface across a varied set of vessels.
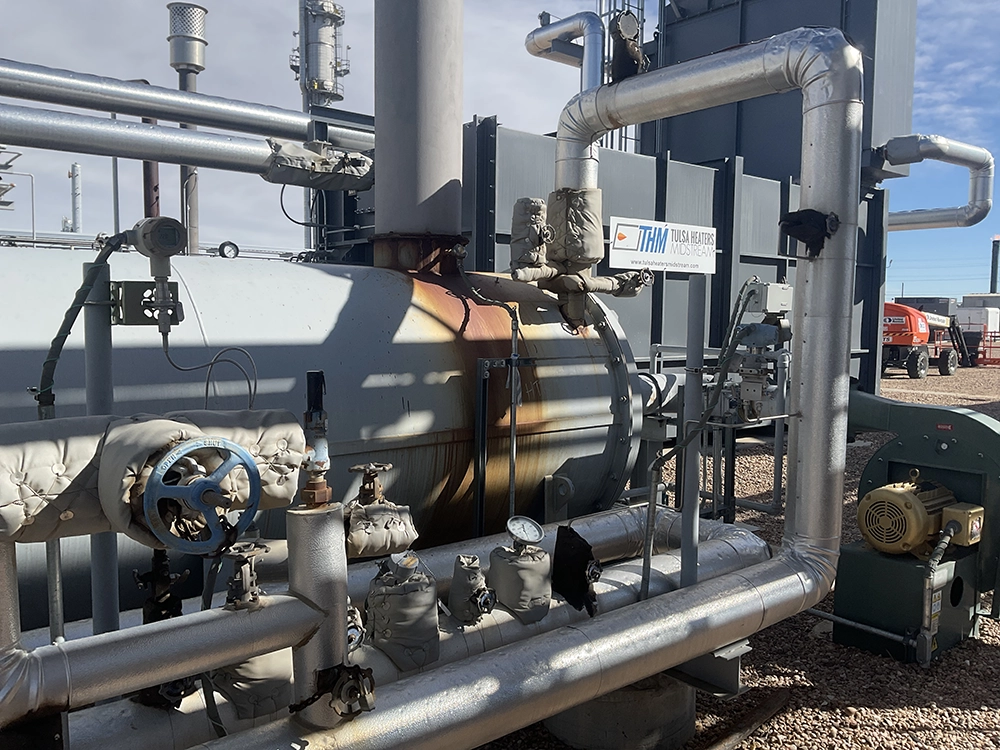
- Fuel train modernization: Profire rebuilt or upgraded every unit’s fuel train, from targeted component swaps to complete rebuilds, all brought up to current NFPA 87 code.
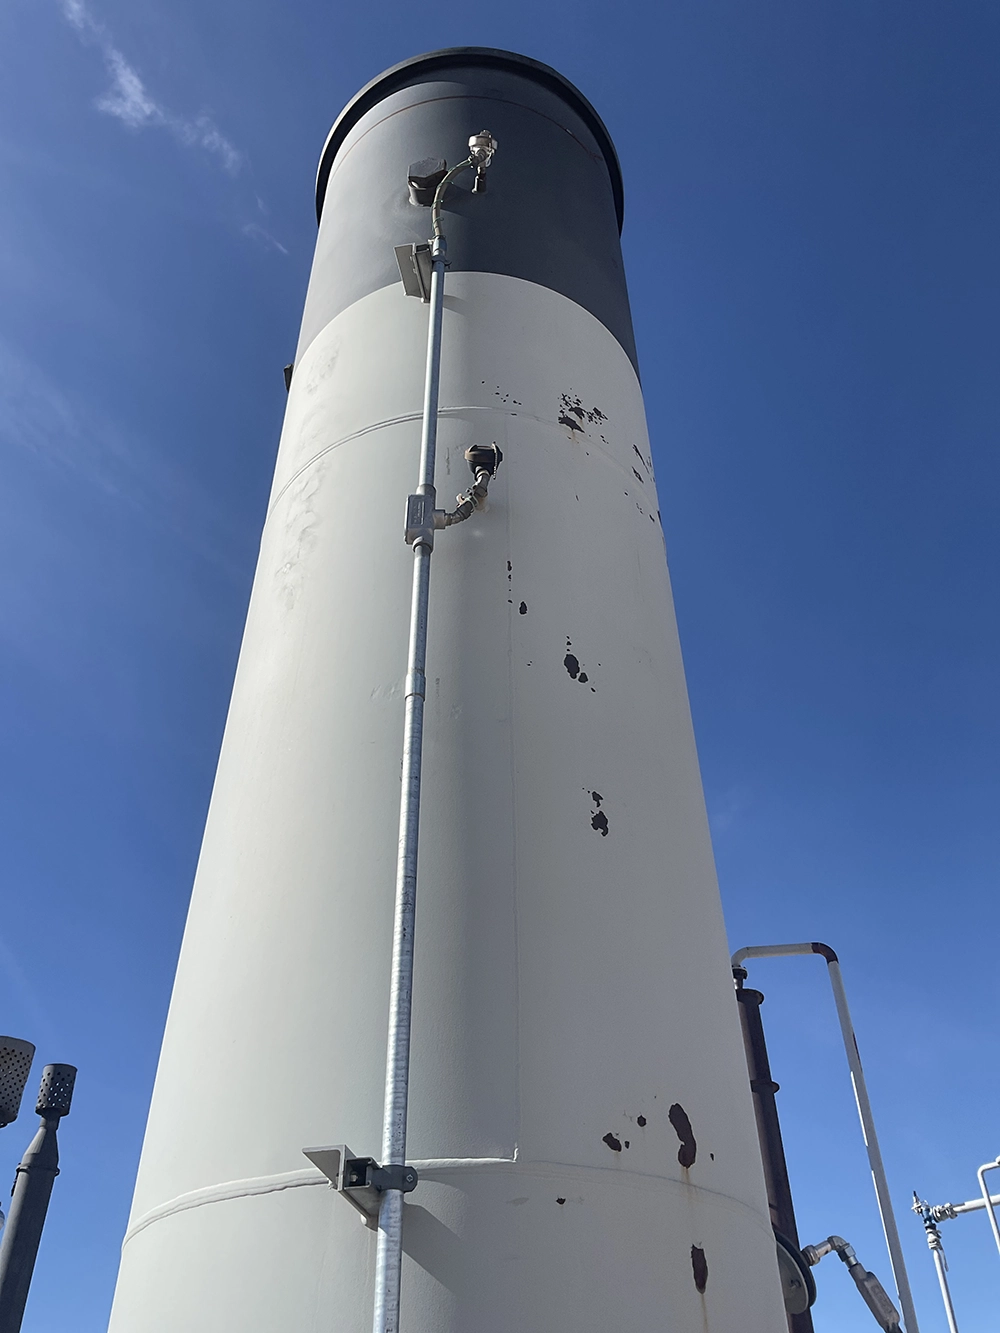
- Burner and pilot scope: New pilots for the two cabin heaters and the thermal oxidizer, and complete burner installs for the two glycol dehydrators.
- Self-checking flame supervision: Flame scanners with self-checking capability as part of a failsafe-by-design approach.
- Control room communication: Modbus to SCADA communication brought up to modern standards so Western can monitor and operate all units from the control room.
- Full-scope delivery: Scope-out, mechanical work, commissioning, startup, tuning, and emissions reporting delivered by Profire as a single source.
The Results:
With all 8 units modernized and running, Western reported positive early results, including no nuisance shutdowns and no outstanding complaints following startup.
The most immediate change was reliability. Replacing aging, inconsistent controls with a uniform PF3100 platform gave operators equipment that started and ran predictably, which reduced the manual intervention the old relight behavior had required. The fuel train upgrades and commissioning tuning also improved burner efficiency across the units.
Consistency proved to be one of the most practical benefits. Because every heater now runs the same panel, operators work from one familiar interface regardless of vessel type, which makes training and troubleshooting easier. It also lets Western stock a common set of spare parts that work across its installed base of heaters rather than managing unit-specific inventory.
Profire is proposing an annual preventive maintenance program to keep the units inspected and running well, giving Western a way to catch potential issues early rather than letting years pass between checks.
Get a Free QuoteAfter Profire
Key Products Used
Ready to Optimize your Equipment?
Let Profire help with your Safety, Reliability, and ESG Initiatives
Get a Free QuoteRecent Projects
Details
See Details
Western Midstream operates a natural gas processing plant near Denver, Colorado that had been running for…
Details
See Details
A leading Oil & Gas producer operated 148 aging dual-tube horizontal heater treaters running on pneumatic…
Details
See Details
At a natural gas utility site in Ontario, a installed Tecvalco CWT Vacuum Heater was exposed…